


Water Pump
Chemical Pump
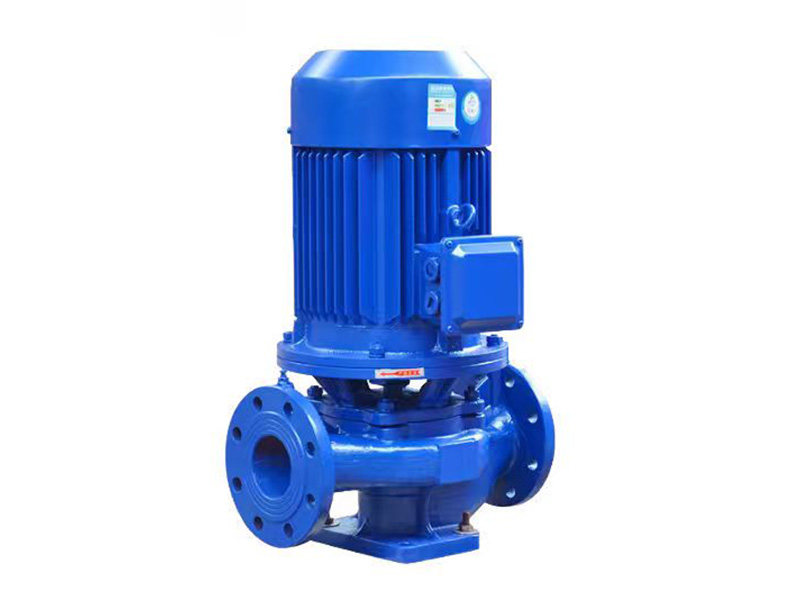
Performance summary
- Flow
- 2.5-550 m3/h
- Head
- 10-150m
- Power
- 0.37-125kw
 Flow
 Head
 Power

Values are from archived product information. Confirm the current model datasheet before selection.
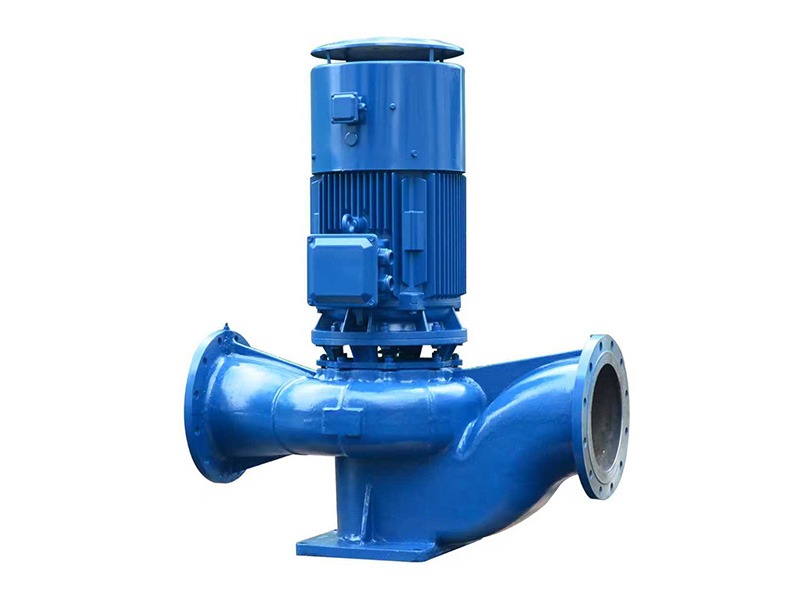
The chemical pump is specially designed for transferring corrosive and aggressive liquids such as acids, alkalis, and chemical solvents. Made of high-quality corrosion-resistant materials, it ensures long service life and stable performance in harsh environments. This pump features high efficiency, low noise, and reliable sealing, making it suitable for continuous operation in chemical plants, wastewater treatment systems, and various industrial applications where safety and precision chemical fluid handling are required.
Main Application Areas1. Chemical PlantsUsed for transporting various acids, alkalis, salts, solvents, and corrosive or volatile chemical media.Typical applications include reactor circulation, chemical raw material transfer, and coolant circulation.2. Pharmaceutical PlantsUsed for transferring liquids in pharmaceutical processes, such as intermediates, extracts, and purified solutions.The pump body material must be corrosion-resistant and non-polluting.3. Water Treatment and Environmental EngineeringUsed for transporting chemical solutions in sewage treatment plants, desalination systems, and acid-base neutralization systems.Suitable for metering and dosing chemical solutions such as sodium hypochlorite, sulfuric acid, and hydrochloric acid.4. Food and Beverage IndustryUsed for transporting chemical solutions such as cleaning agents, disinfectants, and additives.The pump body material must be safe and free of metal leaching contamination.5. Electroplating and Metal Surface Treatment PlantsUsed for circulation and filtration of pickling solutions, alkaline cleaning solutions, and plating solutions.Due to the highly corrosive nature of the media, corrosion-resistant alloys or fluoroplastics are typically used for the pump body.6. Textile and Dye Industry: Transports dye liquor, dyeing auxiliaries, chemical slurries, etc. The pump must be high-temperature resistant, corrosion-resistant, and provide stable output.7. Paper Industry: Transports bleach, additives, alkali, and other chemicals. Commonly used in alkali recovery and bleaching processes.8. Semiconductor and Electronics Industry: Transports ultra-pure chemicals such as hydrofluoric acid, sulfuric acid, and ammonia. Requires no leakage and no metal ion contamination.9. Petroleum Refining and Energy Systems: Transports petrochemical raw materials, additives, and wastewater. Typically requires an explosion-proof motor.10. Laboratories and Research Facilities: Used in small systems for corrosive fluid circulation, reaction fluid transportation, and coolant circulation.2. Typical Usage1. Fixed Installation: Vertically installed in chemical equipment piping, directly connected to the pipe flange to save space.Mostly used in continuous chemical production lines.2. Circulation: Serves as a system circulation pump to maintain fluid circulation in chemical reactions or heat exchange systems.3. Metering and Dosing SystemWorks with flow control devices to precisely deliver corrosive chemicals.4. Cooling and Cleaning SystemUsed for circulating chemical solutions in cooling towers, cleaning tanks, or reaction equipment.5. Anti-corrosion Conveying SystemReplaces traditional cast iron or stainless steel pumps to prevent corrosion when conveying media containing acids, alkalis, and salts.
Related equipment
View category
Need help specifying this pump?
Have your required flow, pressure and application ready for selection.